
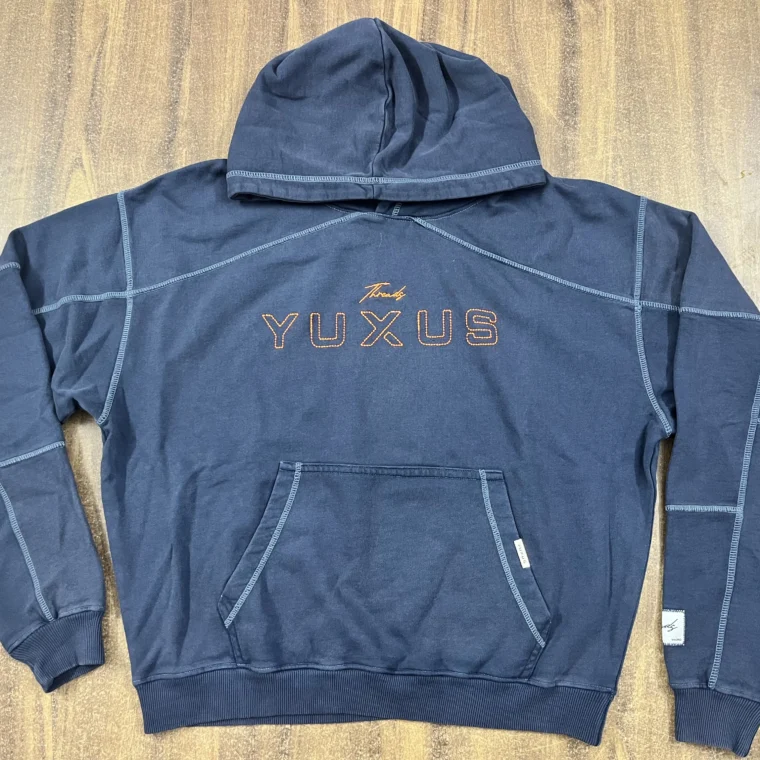

A Manufacturing Analysis of Flatlock vs. Flat Bed Mechanics in Garment-Dye Production. The global shift toward heavyweight streetwear (350GSM and above) has exposed real limits in standard knitwear machinery. This technical report documents a production bottleneck we met with 5-thread flatlock stitching on rigid 400GSM greige French terry, and the mechanical protocol that resolved it. If you are choosing a heavyweight hoodie manufacturer, the lessons below show what to ask before you approve a sample.
The Client Challenge
A premium streetwear brand commissioned a line of 400GSM oversized hoodies. The requirement was simple on paper but difficult in execution. The fabric was 100% cotton French terry at 400GSM, supplied in the greige state (raw and unfinished) so the finished hoodies could be garment dyed. The construction called for a 5-thread flatlock stitch, chosen for its visible, flat seams. Heavy fabric, an unfinished surface, a visible seam, and a dye process that exposes every stitch fault made this a demanding combination, and exactly the kind of programme a good streetwear factory is tested by. Oversized hoodie manufacturers meet this combination less often than their sample rooms suggest.
The “Sample Room” Trap
During sampling, the prototypes passed quality control. Skilled operators working at low speed on single pieces executed the flatlock stitch successfully, which created a false positive. A sample room can compensate for a difficult fabric with operator skill, patience, and hand guidance. A bulk line cannot, because bulk production runs at speed, with many operators, and depends on the machine to do the work consistently.
Once bulk production began, the high-speed feed-off-the-arm (FOA) machines failed. The 400GSM greige fabric, lacking softeners, was too rigid, or “boardy”. The needles began deflecting, which caused skipped stitches and uneven tension that would likely have burst during dyeing.
Why 400GSM Greige French Terry Behaves Differently
| Property | Effect on Stitching |
|---|---|
| High weight and thickness | Seams stack several layers of dense terry, so the needle meets more resistance on every stroke |
| No softener (greige state) | The fabric is stiff and does not relax under the foot, so feed is uneven |
| Loop-backed terry structure | The looped back resists compression and grips unevenly against feed dogs |
| Garment-dye processing | Wet processing and tumbling stress every seam, so a weak stitch fails after dyeing, not before |
Karthik’s Production Protocol
The diagnosis: The standard FOA mechanism could not generate enough grip to feed the rigid 400GSM layers evenly. The solution: We halted the line and re-engineered the process using an industrial flat bed machine. By using a specialised cover-stitch setup with differential feed adjustments, we mimicked the visual appeal of the 5-thread flatlock while providing a stable platform for the heavy fabric.
| Factor | FOA Flatlock (Failed) | Flat Bed Cover Stitch (Passed) |
|---|---|---|
| Fabric support | Fabric hangs off the arm and is pulled through | Fabric lies flat on a stable bed |
| Feed control | Limited grip on rigid layers | Adjustable differential feed |
| Speed | High, which amplifies needle deflection | Controlled to match fabric weight |
| Seam look | True flatlock | Flat, flatlock-style finish |
Technical Results and Data Verification
By switching machinery, we achieved the client’s aesthetic goals without compromising the structural integrity required for the rigorous garment-dye process.
| Metric | Standard Flatlock (Failed) | Flat Bed Solution (Passed) |
|---|---|---|
| Needle deflection | High (frequent skips) | Zero (stable feed) |
| Bursting strength | Unstable | ISO standard compliant |
| Dye penetration | Uneven (white lines) | 100% uniformity |
Garment-Dye Rules for Heavyweight Seams
Garment dyeing adds its own demands, and a premium streetwear manufacturer has to plan for them before cutting, and a high quality streetwear manufacturer treats the seam as part of the dye plan. Thread choice matters: polyester thread does not take cotton dyes, so seams can show contrast after dyeing, which is why dye-compatible cotton or cotton-based thread is normally specified for garment-dyed programmes. Seams also need stitch density and tension that hold under wet processing and tumbling, and dye penetration should be checked on the actual seam, not only on the flat fabric. Greige fabric is later softened during pre-treatment, so the stitch has to be engineered for the fabric as it is on the machine, not as it will feel after dyeing. Our guides to heavyweight hoodie manufacturing cost and fleece and French terry fabrics cover the fabric and cost side of these programmes.
Recommendation for Sourcing Directors
When specifying 400GSM+ programmes intended for garment dyeing, do not rely solely on visual samples. Ensure your tech pack allows for “machinery adaptation”. Rigid greige fabrics need robust feed mechanisms that standard lingerie and sportswear flatlock machines cannot support. Use the checklist below when you evaluate a heavyweight hoodie manufacturer or any streetwear factory.
| Ask the Factory | Why It Matters |
|---|---|
| Was the sample made on the machine used for bulk? | Avoids the false positive from a hand-guided sample |
| Which machines will sew 350GSM+ fabric? | Heavy fabric needs the right feed mechanism |
| What thread is used for garment-dyed styles? | Thread must take the dye or seams will contrast |
| Is seam strength tested after dyeing? | Dye processing is where weak seams fail |
| Does your tech pack allow machinery adaptation? | Lets the factory change the process without a new approval cycle |
Brands building oversized ranges can also see our guide to oversized hoodie manufacturers, and our page for streetwear manufacturers in India shows the wider range of programmes we run.
Planning a Heavyweight Streetwear Hoodie Collection?
The Synerg, Tirupur, India
Avoid production delays by working with a manufacturer that understands the technical science of GSM and garment dyeing. We make heavyweight French terry hoodies and sweatshirts in our own factory in Tirupur with 100 sewing machines, start knit orders at 300 pieces per colour per style, take 75 to 90 days from purchase order to shipment, and inspect every order to AQL 2.5.
Frequently Asked Questions
Why do 400GSM hoodies cause stitching problems?
Heavy, rigid fabric resists the needle and feed mechanism. On high-speed machines this causes needle deflection, skipped stitches, and uneven tension, especially in greige fabric with no softener.
Why do garment-dyed hoodies show white lines on seams?
White lines usually appear where seams are uneven or stitches skipped, so dye cannot penetrate evenly. Correct machinery, stitch settings, and dye-compatible thread prevent it.
What is the difference between flatlock and flat bed stitching?
Flatlock produces a flat, visible seam on specialist machines. A flat bed machine with a cover-stitch setup supports heavy fabric on a stable bed and can reproduce a similar flat finish with better control.
What should a heavyweight hoodie manufacturer be able to show?
A high quality streetwear manufacturer should show samples made on bulk machinery, test results for seam and bursting strength after dyeing, and clear process control for 350GSM+ fabric.
Can a premium streetwear manufacturer garment dye heavyweight hoodies?
Yes, but it needs the right pre-treatment, dye-compatible thread, and seams engineered for wet processing, so ask for a production-machine sample before approving bulk.
About the Author: Karthik Shan
Karthik Shan is the founder and CEO of The Synerg and a manufacturing strategist with 20+ years in Tirupur’s knitwear cluster. He specialises in solving high-complexity production challenges for global streetwear brands.